Mechanical
Review the proposed tag fixing and reader layout with the tool owner. Include tool function, mounting space, handling, cleaning, impact and maintenance access, plus nearby tagged tools at each read point.
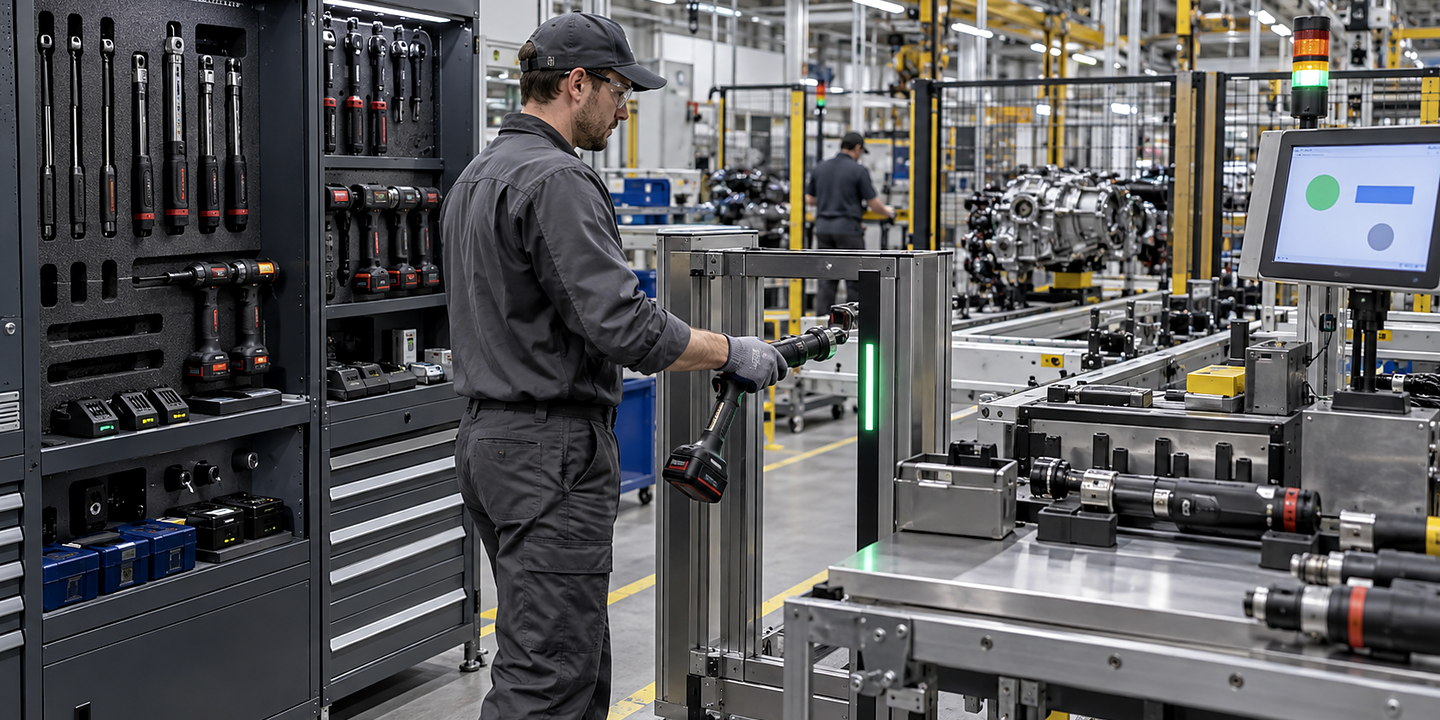
Define RFID mould tracking interfaces for installation, machine and job records, usage sources, maintenance status and controlled interruption recovery.
Connect the confirmed mould configuration to a defined machine, job and installation/removal event. Identify the source of any cycle or operating-hour data and when it applies, then agree record acceptance, interruption recovery and maintenance release responsibilities across the connected systems.
Document the tool, event and configuration fields in the interface brief. RFID identifies the tool; it does not independently measure cycles or establish that production may safely start.
Plan RFID mould tracking around your identifiers, substrates, production events, system interfaces, exceptions and verification records. Discuss a practical data-flow approach with Oxford Traceability. Your integration review should connect production speed and read-point conditions, line, business-system and network interfaces and the people who run the process.
Discuss your application

Review the proposed tag fixing and reader layout with the tool owner. Include tool function, mounting space, handling, cleaning, impact and maintenance access, plus nearby tagged tools at each read point.
List proposed supplies, isolation, protective arrangements and cable routes at stores and machines. Confirm responsible site/electrical teams and external dependencies for the intended installation.
Define how installation and removal are confirmed against the machine and authorised job. Agree the response to wrong tools, unreadable tags and incomplete changes, and assess any proposed permissive separately.
Have the responsible site team review access, tool handling, maintenance and any proposed control changes. A successful RFID read or identity match does not establish safe installation or permission to run.
Agree mould/insert/configuration/job/event fields, usage sources, start/stop rules and counter resets. Define acceptance, rejection, delayed records and interruption recovery while preserving earlier run history.
Name who resolves discrepancies, replaces tags, confirms configuration changes and releases tools from maintenance. Train the controlled manual/correction route and retain the original discrepancy and reason for changes.
For RFID Mould Tracking, your team can review each stage before the complete installation is put into routine use.
Share real identifiers, substrates, production events and exception records, including the normal range for identifier and data rules for RFID identification of production moulds and the difficult substrate, label or tag behaviour cases.
Compare suitable methods and use focused trials to show how each option performs against production speed and read-point conditions.
Connect the equipment to your line, services and controls while resolving line, business-system and network interfaces for day-to-day operation.
Confirm exception, rework and duplicate handling, then complete and record verification, retention and reconciliation evidence before your operating team takes over.
For your application: check production speed and read-point conditions, line, business-system and network interfaces, exception, rework and duplicate handling, and verification, retention and reconciliation evidence as part of the complete line trial.